
ISO 2858 Horizontal Centrifugal Chemical Process Pump
Standardized back pull-out centrifugal chemical pumps providing leak-free reliability, low NPSH requirements, and exceptional resistance to sulfuric, nitric, and hydrochloric acids in chemical and petrochemical plants.
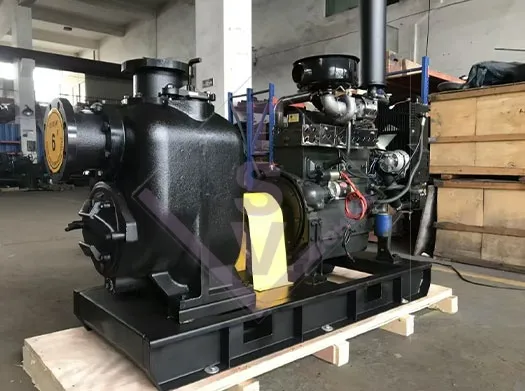
Design Criteria & Manufacturing Specifications
Manufactured strictly to international pumping machinery standards with 100% factory hydrostatic shell testing, dynamic rotor balancing, and certified performance testing per ISO 9906 / API 610.
| Engineering Parameter | Applicable Codes, Standards & Design Criteria |
|---|---|
| Design Standards | ISO 2858, ISO 5199, EN 22858, ASME B73.1 |
| Flange Ratings & Connections | EN 1092-2 PN 16/25, ASME B16.5 Class 150/300 RF |
| Operating Flow Capacity | Up to 1,500 m³/h (6,600 GPM) |
| Total Dynamic Head | Up to 160 meters (525 feet) |
| Shaft Sealing Options | Cartridge Single / Dual Mechanical Seal, API Plan 11/52/53 Flush |
| Wet-End Metallurgy | ASTM A351 CF8M, CF3M, 904L, Titanium Gr.2, Hastelloy C-276 |
| Design Pressure & Temp | 16 bar to 25 bar design; Temperature from -40°C to +260°C |
| Testing & Acceptance | ISO 9906 Grade 1B/2B Hydrostatic Shell & Hydraulic Performance Test |
ISO 2858 Chemical Process Pump Standard & Engineered Models
Browse TSV's complete portfolio of end-suction, magnetic-drive, and severe-corrosion chemical process pumps engineered for chemical refineries and chlor-alkali production.
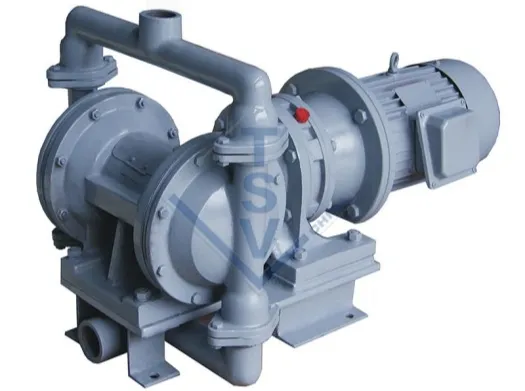
ISO 2858 Standard Mechanical Seal Chemical Process Pump
Heavy-duty horizontal end-suction centrifugal pump with modular back pull-out construction allowing rapid maintenance without piping disconnection.
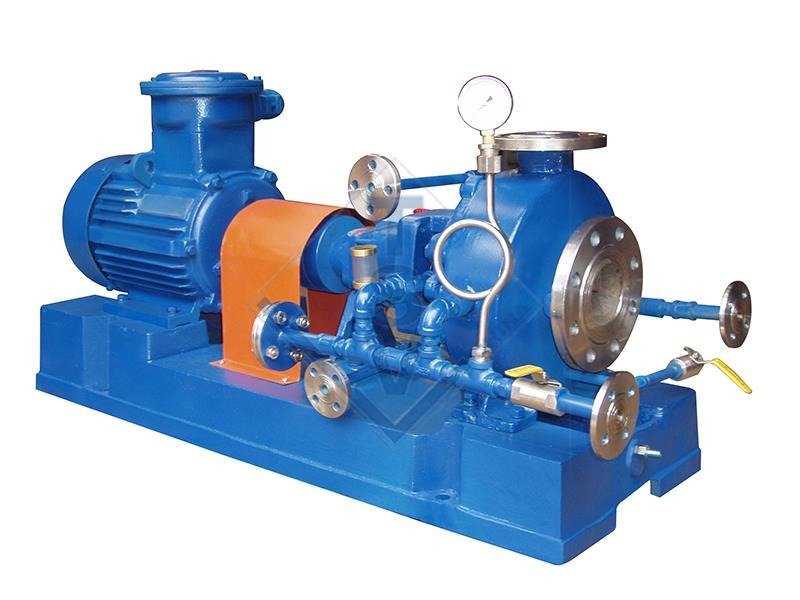
Zero-Leakage Magnetic Drive Sealless Chemical Process Pump
Hermetically sealed mag-drive pump utilizing rare-earth samarium-cobalt magnets, totally eliminating mechanical seal leakage on hazardous and toxic media.
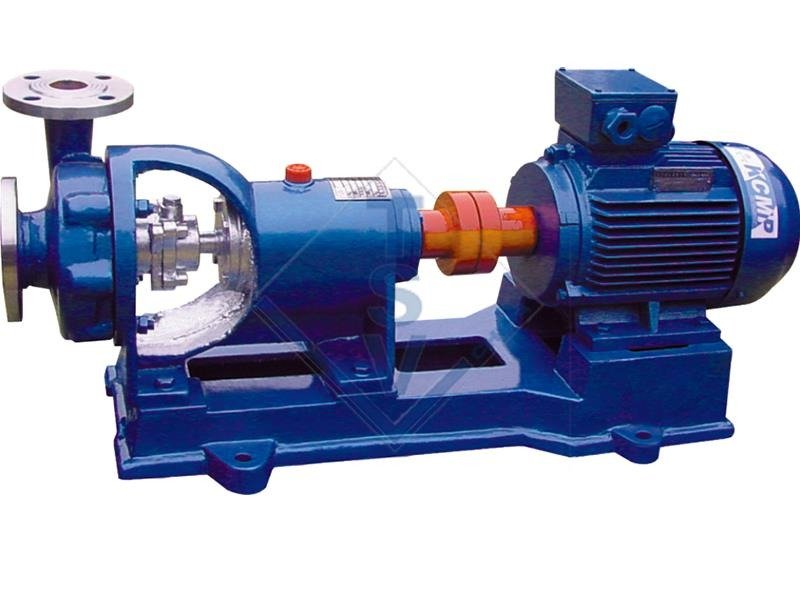
Severe Acid Titanium & Hastelloy High-Alloy Process Pump
Engineered wet-end forged from solid Titanium Gr.2 or Hastelloy C-276 for handling boiling hydrochloric acid, wet chlorine gas, and aggressive pickling liquors.
ISO 2858 Chemical Hydraulic Architecture & Shaft Sealing Integrity
Engineered to deliver hydraulic efficiency exceeding 82% while guaranteeing absolute containment of hazardous volatile chemicals.
Modular Back Pull-Out Maintenance
Allows complete bearing frame, impeller, and mechanical seal extraction towards the motor side without disturbing suction or discharge pipeline flanges.
Precision Dynamically Balanced Impeller
Closed radial flow impeller dynamically balanced to ISO 1940 Grade G2.5, minimizing shaft deflection and extending mechanical seal MTBF to > 25,000 hours.
Engineered Heavy-Duty Bearing Frame
Enlarged oil reservoir with non-contact labyrinth bearing isolators (IP66) and magnetic drain plug, preventing lubricant contamination by corrosive atmospheric vapors.
Explore All 4 Industrial Process Pump Sub-Categories
1:1 aligned with TSV factory catalog. Navigate to chemical end-suction, API 610 refinery, high-pressure multistage, or heavy-duty slurry pumps.
ISO 2858 Chemical Process Pump
End-suction centrifugal process pumps engineered for aggressive acids, caustic chemicals, and petrochemicals.
Current Series View Page Top ↑API 610 Petrochemical Pump
Heavy-duty OH2 / BB2 process pumps for extreme temperature refinery hydrocarbons and high-pressure duties.
API 610 11th / 12th View Details →Multistage Boiler Feed Pump
High-pressure ring-section and horizontal split-case feed water pumps for thermal power plants and steam boilers.
High Pressure Feed View Details →Heavy Duty Slurry Pump
Abrasion-resistant centrifugal slurry pumps with high-chrome liners for mineral processing and tailings.
Heavy Slurry Duty View Details →Configure & Request a Quote for ISO 2858 Horizontal Centrifugal Chemical Process Pump
Submit your process hydraulic parameters and fluid properties. TSV application engineers provide complete pump selection datasheets, motor sizing curves, and official quotation within 24 hours.